The welded base and side frames support the working assemblies and maintain the machine layout.
 Long Panel Bending


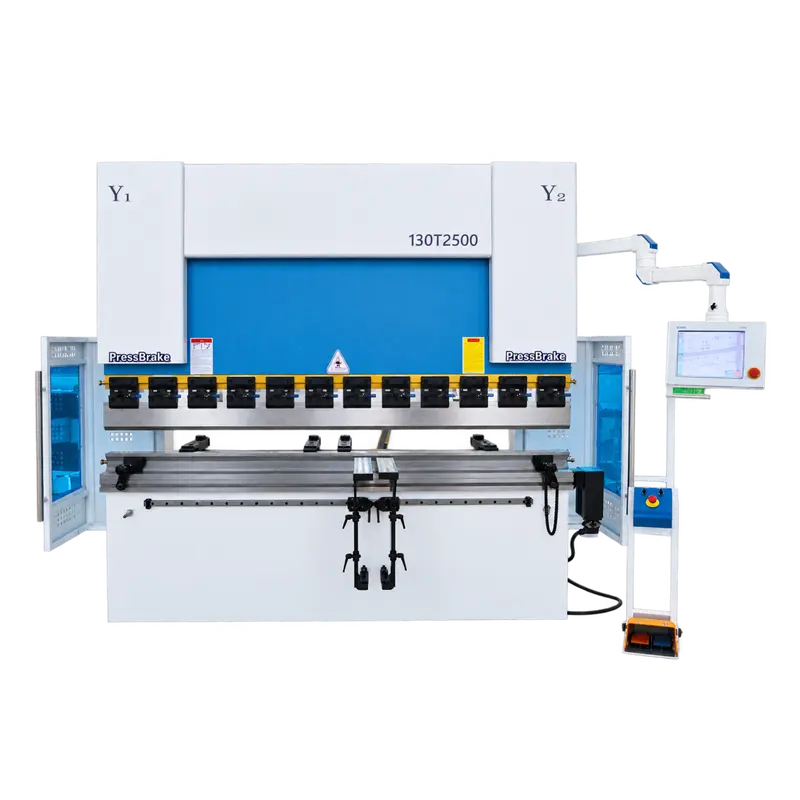
Electro-Hydraulic Servo CNC Press Brake
Suitable for metal fabrication shops, enclosure and cabinet production, HVAC duct work, equipment manufacturing, and contract bending services, this press brake forms flat sheet into panels, brackets, channels, and long profiles. It can be arranged with suitable segmented tooling, front supports, programmed backgauge positions, and crowning adjustment for prototypes, mixed batches, or repeat production.
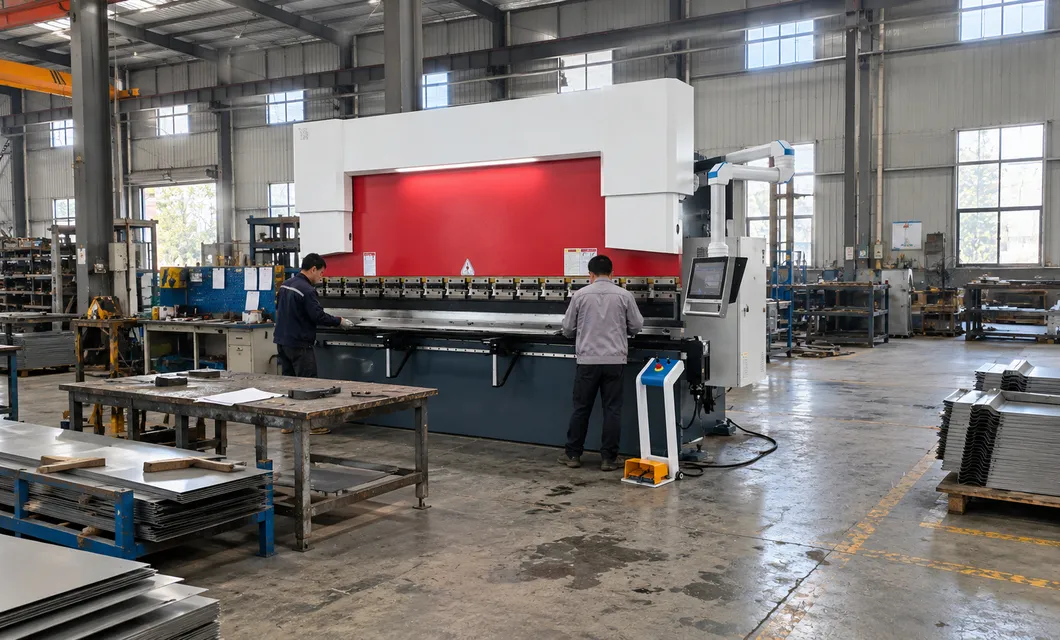 Control Station Setup
 Sheet PositioningLong Panel Bending
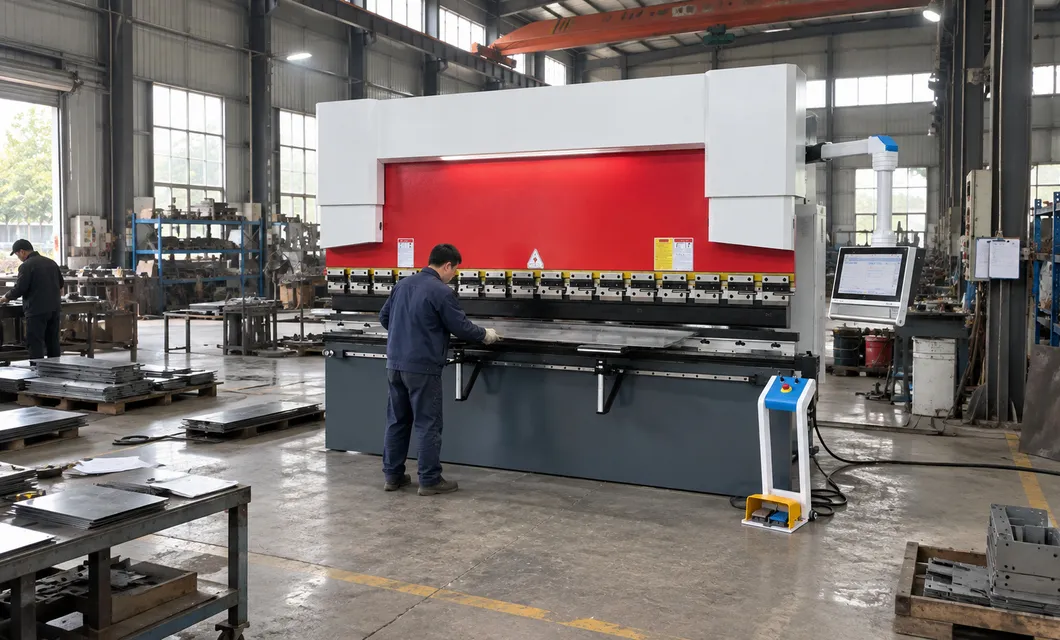 Workshop ProductionControl Station SetupSheet Positioning
The backgauge moves along guides to establish a stable sheet position, supporting efficient adjustment for different bending sizes.
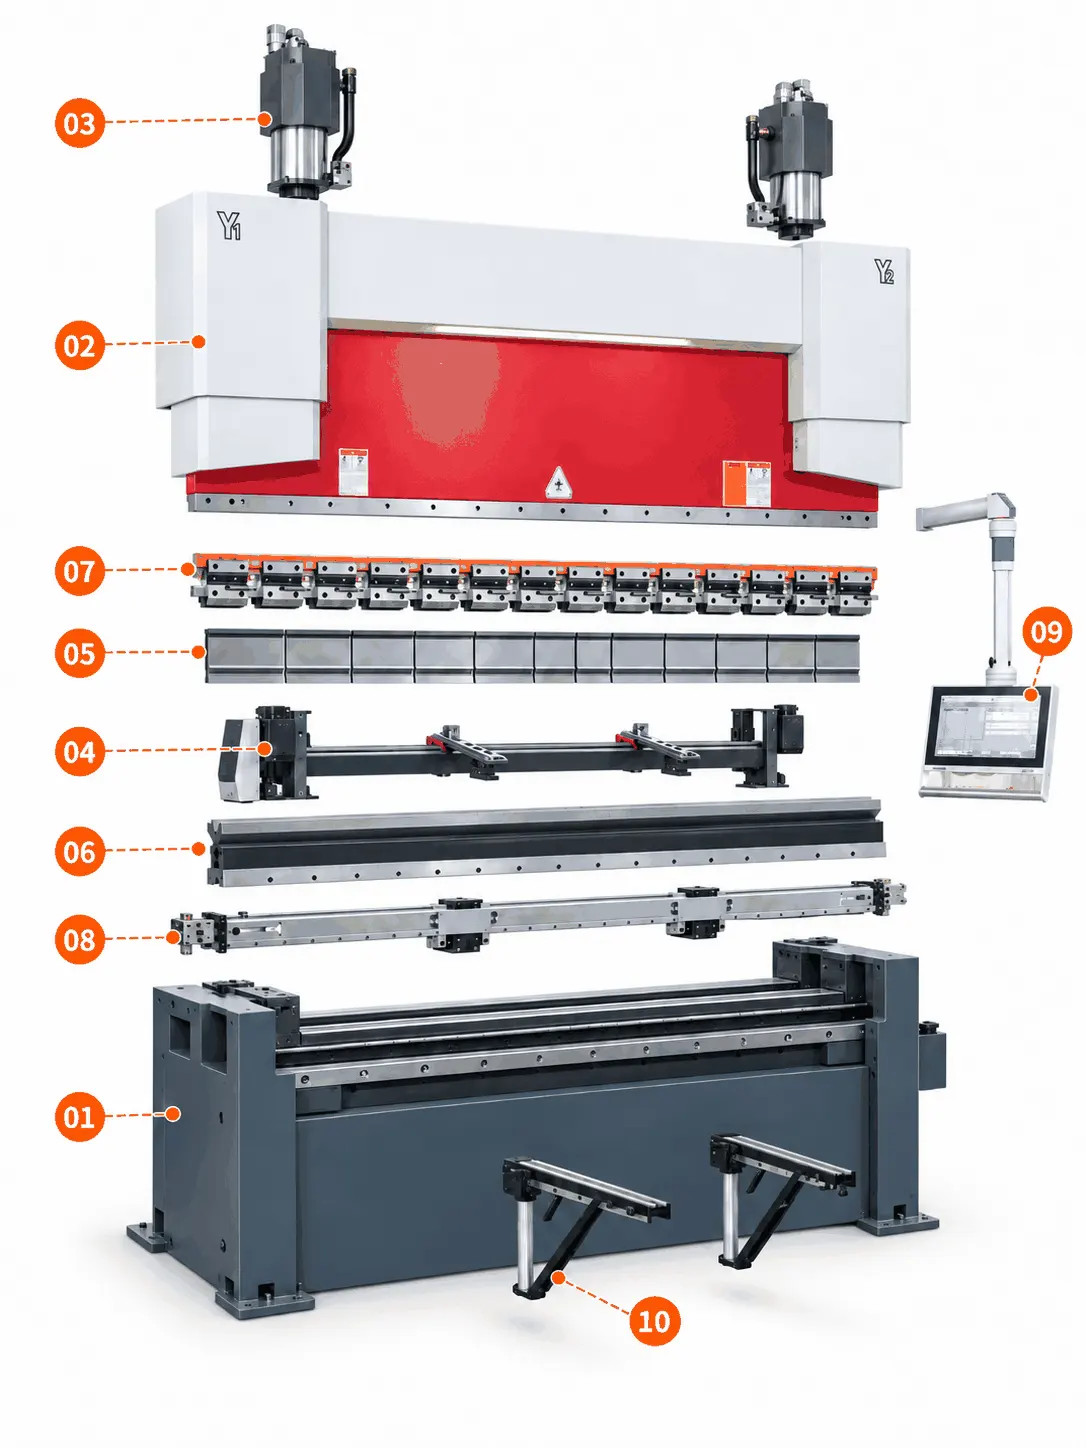
The welded base and side frames support the working assemblies and maintain the machine layout.
The moving ram carries the upper tooling and transfers cylinder motion through the bending stroke.
Two hydraulic cylinders drive the ram and work with position feedback for synchronized movement.
The rear backgauge uses guided motion to position sheet edges for programmed bend locations.
Segmented upper tooling can be arranged along the ram to suit different part widths and profiles.
The combination lower die provides selectable V openings for common sheet-metal forming tasks.
Mechanical quick clamps secure punch segments while supporting practical tooling changes.

DA53T Electro-hydraulic Servo machine display. Servo drive, powerful output and high control accuracy.
00:50DA53T Electro-hydraulic Servo machine display. Servo drive, powerful output and high control accuracy.
01:13DA53T Electro-hydraulic Servo operation demo. Fast response, stable running and excellent machining precision.
Real on-site records from our factory, offering a practical view of our production capability and delivery readiness.
Each unit is checked before delivery against the following inspection items.
Our team is ready to advise you on the best product configuration and procurement plan.
info@eascoutia.com400 158 5899It is intended for sheet-metal panels, brackets, channels, and profiles within the verified capacity and suitable tooling range.
The supplied configuration uses Y1 and Y2 for ram motion, X and R for the backgauge, and W for mechanical crowning.
Segmented upper tooling, a combination lower die, and mechanical quick clamps are arranged for the required bend profile.
Operators can reuse programmed positions and backgauge settings after confirming the tooling arrangement for the current job.
Provide material type, thickness, part length, bend drawing, required profile, and expected batch quantity for selection.
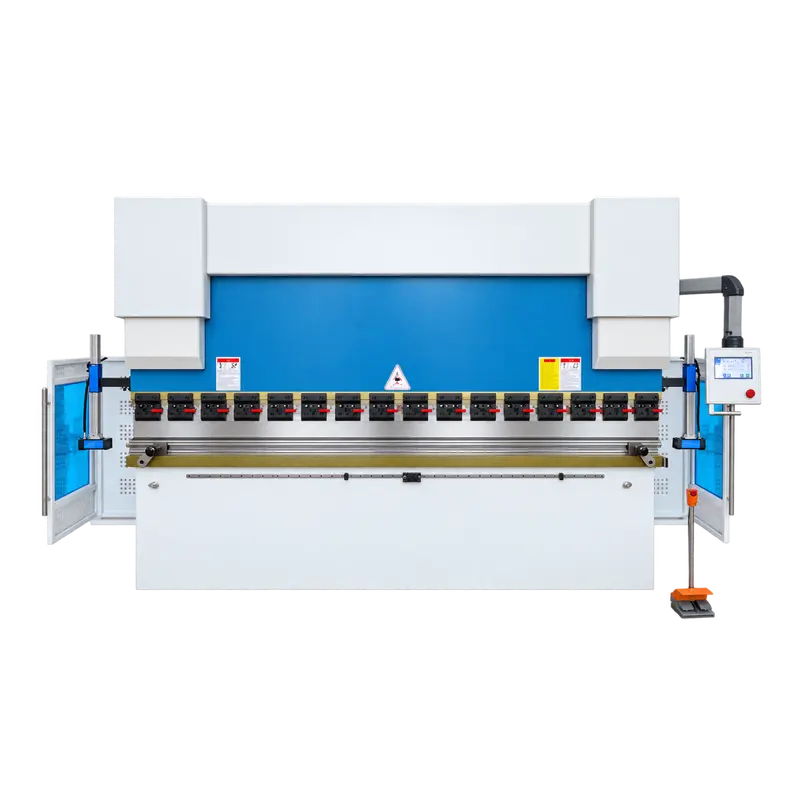


 Simplified explanation
